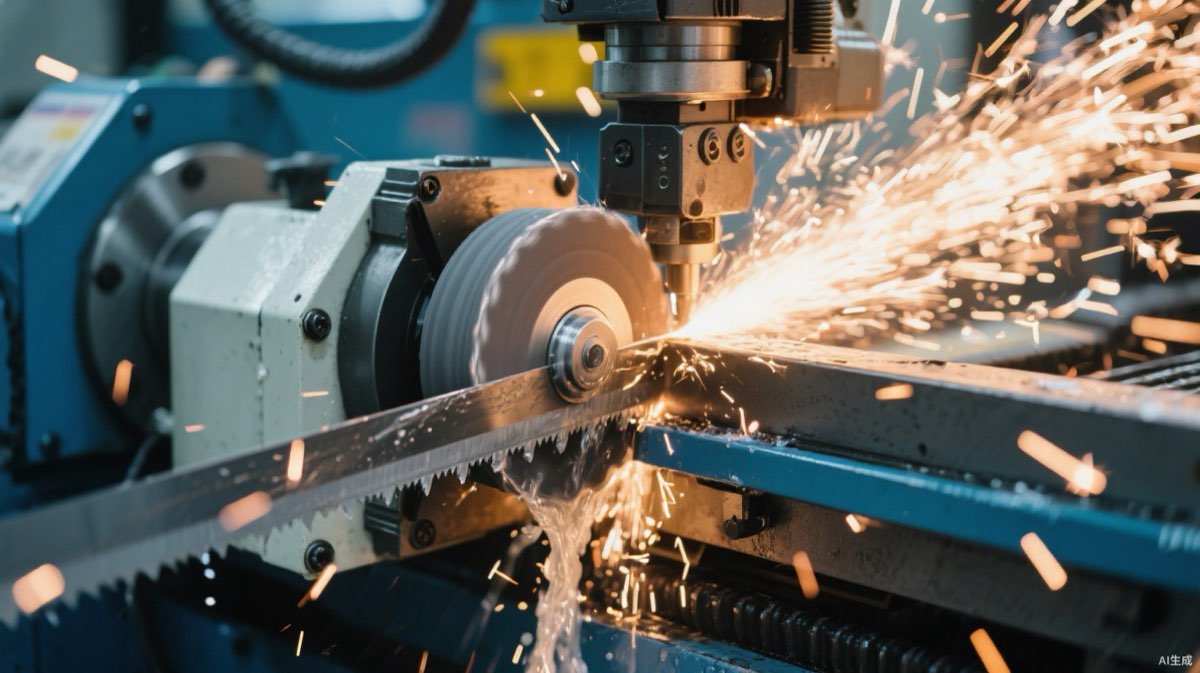
A circular slitter blade can typically be reground 3–5 times before it must be replaced. Whether each regrind makes sense is simple arithmetic.
First, diameter budget. Every regrind removes 0.3–1.0 mm of diameter. Your machine has a minimum diameter at which blade-to-anvil or blade-to-blade clearance can no longer be set. Count your remaining regrinds against that budget.
Second, geometry limits. Blades with complex edge profiles — zigzag cutters, crush cutters, toothed knives — lose their geometry faster and cost more to reprofile. Sometimes two regrinds is the realistic maximum.
Third, downtime math. If a blade set costs $400 and lasts a month between regrinds, but an unexpected blade failure stops your line for four hours at $2,000/hour, the risk-adjusted answer is to regrind on schedule, never to run blades to failure.
We offer regrinding services with original-spec inspection, and we keep dimension records for every blade we sell — so reorders and regrinds match your first set exactly.